Every figure below is taken from a resin manufacturer’s own processing guide or technical data sheet. A source note is at the bottom. Where two suppliers disagree materially, both numbers are shown rather than averaged, because averaging two vendors’ specs produces a number neither of them stands behind.
Always verify against the data sheet for the specific grade you are running. These are family-level typical values. Fillers, impact modifiers, flame retardants and colorants all move the numbers.
Sizing a dryer or hopper? Use the dryer and hopper calculator. Want this on the wall by the press? Print the drying chart.
First: hygroscopic is not the same as hydrolysis-sensitive
This distinction explains why ABS tolerates 0.1% moisture while polycarbonate demands 0.02%, and it is the single most useful thing to understand about drying.
- Hydrophobic: PE, PP, PS, PVC. They pick up surface moisture only, which seldom exceeds 0.01%. Drying is usually unnecessary.
- Hygroscopic, cosmetic consequences: ABS, SAN, ASA, acrylic, PPE, POM. They absorb water and mold with splay if wet, but the polymer backbone survives. Most tolerate 0.05–0.10%; modified PPE and optical acrylic need 0.02% or less.
- Hygroscopic, performance consequences: PET, PC, nylon, PBT, TPU, PEI. Water at molding temperature cleaves the polymer chain. The damage is permanent and the limits are tight: about 0.02% for PC, PET, PBT and PEI, up to about 0.05% for TPU, and 0.2% or less for nylon.
Companion chart: melt temperature, mold temperature and shrinkage by resin
Desiccant dryers are usually run at a dew point of about −40°C / −40°F or drier. A dryer that cannot hold its dew point will not reach the moisture targets below, however long the material sits in it.
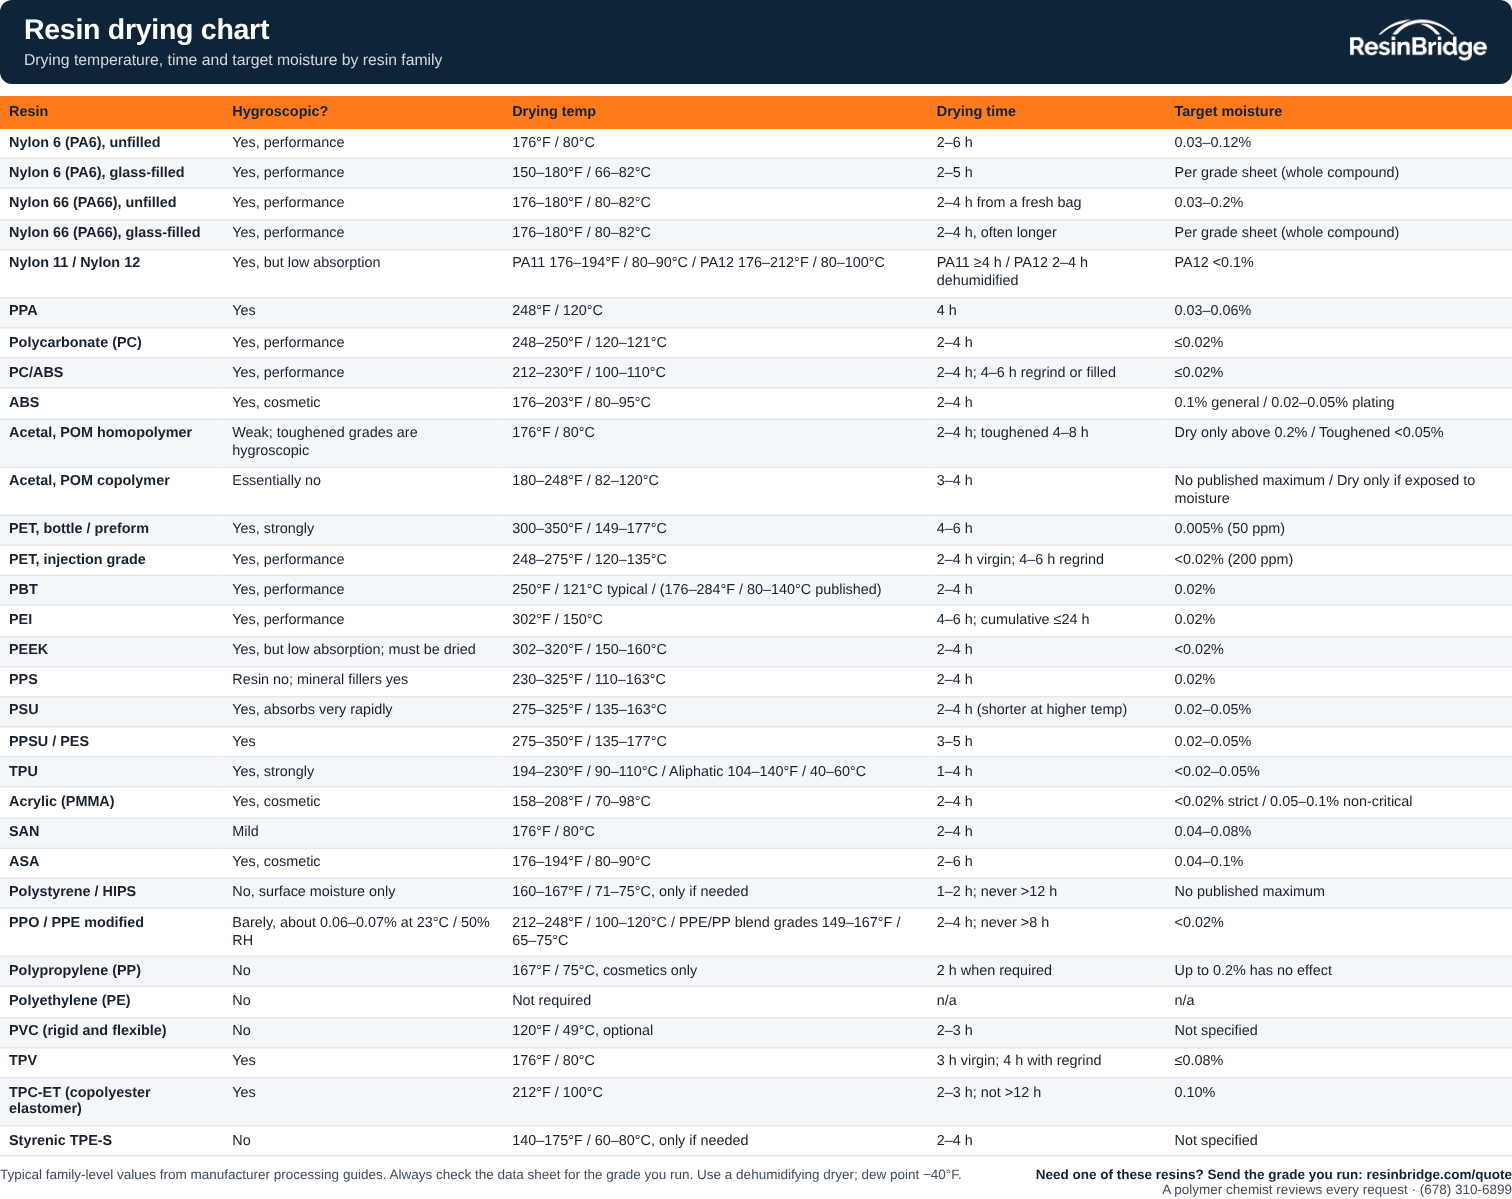
Drying reference chart
Scroll the table sideways to see all columns.
| Resin | Hygroscopic? | Drying temp | Drying time | Target moisture | Notes |
|---|---|---|---|---|---|
| Nylon 6 (PA6), unfilled | Yes, performance | 176°F / 80°C | 2–6 h | 0.03–0.12% | Published targets range from 0.03–0.06% up to 0.12%, depending on producer. Nylon 6 & 66 grades › |
| Nylon 6 (PA6), glass-filled | Yes, performance | 150–180°F / 66–82°C | 2–5 h | Per grade sheet; see note 3 | Producer sheets quote the limit on the whole compound. Scaled to the polymer share it is about 0.08% at 30% GF, 0.07% at 40%, 0.06% at 50%. See note 3. Glass-filled nylon grades › |
| Nylon 66 (PA66), unfilled | Yes, performance | 176–180°F / 80–82°C | 2–4 h from a fresh bag | 0.03–0.2% | One producer’s guide gives 0.03–0.06%; another allows <0.2%, tightening to 0.1% above 600°F melt. Nylon 6 & 66 grades › |
| Nylon 66 (PA66), glass-filled | Yes, performance | 176–180°F / 80–82°C | 2–4 h, often longer | Per grade sheet; see note 3 | One producer’s guide: filled and impact-modified grades “may be longer.” Glass-filled nylon grades › |
| Nylon 11 / Nylon 12 | Yes, but low absorption | PA11 176–194°F / 80–90°C PA12 176–212°F / 80–100°C | PA11 ≥4 h PA12 2–4 h dehumidified | PA12 <0.1% | No injection-molding moisture limit is published for PA11. One producer caps dry air at 80°C (yellowing above); go higher only with dehumidified or vacuum drying. Nylon 11 & 12 grades › |
| PPA | Yes | 248°F / 120°C | 4 h | 0.03–0.06% | Keep the dryer at or below 275°F / 135°C. PPA grades › |
| Polycarbonate (PC) | Yes, performance | 248–250°F / 120–121°C | 2–4 h | ≤0.02% | Some optical and lighting programs set a tighter in-house limit. Polycarbonate (PC) grades › |
| PC/ABS | Yes, performance | 212–230°F / 100–110°C | 2–4 h; 4–6 h regrind or filled | ≤0.02% | Dry to 0.02% or less. Some grades call for 0.01%, so check the data sheet for your grade. PC/ABS grades › |
| ABS | Yes, cosmetic | 176–203°F / 80–95°C | 2–4 h | 0.1% general 0.02–0.05% plating | Moisture causes splay but does not cleave the backbone. ABS grades › |
| Acetal, POM homopolymer | Weak; toughened grades are hygroscopic | 176°F / 80°C | 2–4 h; toughened 4–8 h | Dry only above 0.2% Toughened <0.05% | Standard grades generally do not require drying; toughened grades do. Acetal (POM) grades › |
| Acetal, POM copolymer | Essentially no | 180–248°F / 82–120°C | 3–4 h | No published maximum Dry only if exposed to moisture | Can normally be molded as received. Acetal (POM) grades › |
| PET, bottle / preform | Yes, strongly | 300–350°F / 149–177°C | 4–6 h | 0.005% (50 ppm) | Dew point −40°F / −40°C or lower. Crystallize amorphous regrind first; see note 4. PET / PBT grades › |
| PET, injection grade | Yes, performance | 248–275°F / 120–135°C | 2–4 h virgin; 4–6 h regrind | <0.02% (200 ppm) | Above 0.02% strength drops with no visible surface defect. PET / PBT grades › |
| PBT | Yes, performance | 250°F / 121°C typical (176–284°F / 80–140°C published) | 2–4 h | 0.02% | Some suppliers permit 0.04–0.05%. Drop to 200–212°F / 93–100°C for overnight residence. PET / PBT grades › |
| PEI | Yes, performance | 302°F / 150°C | 4–6 h; cumulative ≤24 h | 0.02% | Published guidance caps total drying at 24 h. PEI grades › |
| PEEK | Yes, but low absorption; must be dried | 302–320°F / 150–160°C | 2–4 h | <0.02% | Absorbs about 0.1% in 24 h and up to about 0.5% at saturation. Dryer dew point −40°F / −40°C. Tray depth ≤1 in. PEEK / PEK grades › |
| PPS | Resin no; mineral fillers yes | 230–325°F / 110–163°C | 2–4 h | 0.02% | About 50°C between suppliers, one of the widest spreads here. Follow your grade’s sheet. PPS grades › |
| PSU | Yes, absorbs very rapidly | 275–325°F / 135–163°C | 2–4 h (shorter at higher temp) | 0.02–0.05% | Published targets are 0.05% and 0.02%, depending on producer. PSU / PPSU grades › |
| PPSU / PES | Yes | 275–350°F / 135–177°C | 3–5 h | 0.02–0.05% | Absent from every dryer-OEM chart; use resin-maker data only. PSU / PPSU grades › |
| TPU | Yes, strongly | 194–230°F / 90–110°C Aliphatic 104–140°F / 40–60°C | 1–4 h | <0.02–0.05% | Hardness- and chemistry-dependent. Use within 15–30 min of the dryer. TPU grades › |
| Acrylic (PMMA) | Yes, cosmetic | 158–208°F / 70–98°C | 2–4 h | <0.02% strict 0.05–0.1% non-critical | Grade-dependent. One producer’s rule: 10–15°C below the Vicat softening point. Acrylic (PMMA) grades › |
| SAN | Mild | 176°F / 80°C | 2–4 h | 0.04–0.08% | Published as a range, not a maximum. ASA / SAN grades › |
| ASA | Yes, cosmetic | 176–194°F / 80–90°C | 2–6 h | 0.04–0.1% | 0.04–0.1% depending on producer. Cumulative max 12 h. ASA / SAN grades › |
| Polystyrene / HIPS | No, surface moisture only | 160–167°F / 71–75°C, only if needed | 1–2 h; never >12 h | No published maximum | Dry only for regrind, humid storage or abnormal conditions. GPPS & HIPS grades › |
| PPO / PPE modified | Barely, about 0.06–0.07% at 23°C / 50% RH | 212–248°F / 100–120°C PPE/PP blend grades 149–167°F / 65–75°C | 2–4 h; never >8 h | <0.02% | PPE/nylon alloy grades have a two-sided window: too dry (<0.02%) also causes splay. PPO / PPE grades › |
| Polypropylene (PP) | No | 167°F / 75°C, cosmetics only | 2 h when required | Up to 0.2% has no effect | Filled and reinforced PP grades are moisture-sensitive. Polypropylene (PP) grades › |
| Polyethylene (PE) | No | Not required | n/a | n/a | Warm-air surface-moisture removal only if condensation is present. Polyethylene (PE) grades › |
| PVC (rigid and flexible) | No | 120°F / 49°C, optional | 2–3 h | Not specified | Most PVC compounds ship ready to process. PVC grades › |
| TPV | Yes | 176°F / 80°C | 3 h virgin; 4 h with regrind | ≤0.08% | TPE / TPV grades › |
| TPC-ET (copolyester elastomer) | Yes | 212°F / 100°C | 2–3 h; not >12 h | 0.10% | Some producers specify ≤0.05%. |
| Styrenic TPE-S | No | 140–175°F / 60–80°C, only if needed | 2–4 h | Not specified | Pre-drying generally unnecessary. TPE / TPV grades › |
Use this chart on your site or print it
Molding schools, dryer and auxiliary equipment dealers, and plants are welcome to put this chart on their own site or intranet. Paste the code below into any page. The chart stays current when we update it, and the credit link has to stay in place. Please don’t change the numbers.
Prefer paper? Download the printable PDF. Want to link instead? Use https://resinbridge.com/insight-resin-drying-guide.
Seven things the chart cannot tell you
1. Over-drying is a real defect
“When in doubt, dry longer” is wrong for several families. One nylon producer prints on its data sheets that excessive drying “may lead to an increase of melt viscosity during processing.” Another: “Do not overdry; it will discolor the nylon.” Published guidance caps modified PPE at 8 hours and cumulative PEI drying at 24. HIPS should not be dried beyond 12 hours. One PPS producer warns against over-drying: long, hot drying oxidizes the resin and raises its viscosity.
2. The post-dryer window is 15 to 30 minutes
One producer notes that for ABS, “as little as 15 minutes of exposure on a humid day can cause moisture defects.” One polycarbonate guide limits unheated hopper residence to 30 minutes. TPU should be used within 15–30 minutes. The same polycarbonate guide adds a subtler trap: conveying dried resin with cold atmospheric air re-wets it; convey with hot dry air off the dryer.
3. Glass-filled nylon: follow the grade sheet, and know the scaled figure
Producer data sheets quote the moisture limit on the whole compound, usually about 0.1–0.2% for glass-filled PA66 (one 30% glass grade lists 0.15%). Glass does not absorb water, though, so a 0.2% reading on a 30% glass-filled grade means the polymer itself is at about 0.29%, and some guides scale the limit down by polymer content. From a 0.2% limit: 0.14% at 30% GF, 0.12% at 40%, 0.10% at 50%. From PA6’s 0.12%: about 0.08%, 0.07% and 0.06%. Use the sheet’s figure as the rule and the scaled one as a tighter target for critical parts, and avoid drying past it, which yellows nylon. One published case describes a 43% glass-filled PA66 molded at its data-sheet 0.2% losing 20% of its intrinsic viscosity.
4. PET regrind must be crystallized before it is dried
Amorphous PET goes tacky around 80°C / 175°F and clumps; the clumps do not break up as temperature rises, and they bridge in the hopper and coat thermocouples. Crystallize first with mechanical agitation, then dry. Clear regrind is amorphous; white regrind is already crystalline. Crystallizing is not drying. Recrystallized PET still has to be dried afterward. For PET chips bought by IV, see PET intrinsic viscosity grades.
5. Nylon goes dryer to press, with nothing in between
One nylon molding guide states that remote tray ovens with manual transfer to the hopper are “not recommended,” and that no more than one hour’s supply should sit in the hopper. Its exposure ladder is worth memorizing: a fresh bag needs 3 hours of drying, a bag left open several days needs 20, and regrind stored in non-moisture-proof containers needs 60. And never use a circulating or fresh-air oven. Another producer warns that in the extreme case “the granules can contain more moisture after drying than they did beforehand.” For nylon chips dried for spinning, see nylon fiber and monofilament resin.
6. Regrind and colorant change the numbers
One producer’s guide: doubling particle weight increases drying time roughly 60%. Regrind and glass-filled PC/ABS goes from 2–4 hours to 4–6. TPV goes from 3 hours to 4. And masterbatch should be tumble-blended with the resin before drying, not after. Four producers’ guides say so independently.
7. You may not be able to measure the tightest specs on your floor
One producer’s assessment: no shop-floor weighing system can reproducibly determine residual moisture below 0.05%. Hitting 0.01–0.02% verifiably requires Karl Fischer or the carbide method. Analyzer setpoints are also resin-specific: one producer specifies 200°C for standard PEEK but 224°C for its higher-temperature PEEK grade, and 170°C for sulfones. A wrong setpoint gives a passing reading on wet resin.
A note on dryer-manufacturer charts
Several dryer manufacturers publish resin charts, and they are useful cross-checks. Two cautions. One widely used chart has an “Initial Moisture %” column that is as-supplied incoming moisture, not a target, and it is widely misread as a spec. And vacuum-dryer charts give cycle times in minutes, which are not comparable to desiccant hours. When an equipment chart and a resin maker’s guide disagree, the resin maker wins.
Common questions
What temperature should nylon be dried at?
About 80–82°C / 176–180°F for both PA6 and PA66, typically 2 to 4 hours from a freshly opened bag. Do not exceed about 93°C / 200°F for long periods, because producer guidance warns it discolors nylon. Never use a circulating or fresh-air oven for nylon: in humid conditions the pellets can leave the oven wetter than they went in.
Can you over-dry resin?
Yes, and it is a real defect for several families. Excessive drying raises melt viscosity in nylon and discolors it. Modified PPE should not be dried beyond 8 hours, HIPS beyond 12, and published guidance caps cumulative drying of PEI at 24 hours.
Why do parts molded from wet resin sometimes look perfect?
Because hydrolysis uses up the water by splitting polymer chains instead of forming surface defects. One producer’s guide describes wet-molded PBT as optically flawless but brittle. A PET guide says the same: strength and toughness drop with no visible surface defect.
Does polypropylene need to be dried?
Normally no. Polypropylene is not hygroscopic, and moisture up to about 0.2% does not affect molded part properties. The exceptions are highly cosmetic parts, filled or reinforced grades, and condensation from cold storage.
How long can dried resin sit before molding?
About 15 to 30 minutes, less on a humid day. One producer notes that as little as 15 minutes of exposure on a humid day can cause moisture defects in ABS. One polycarbonate guide limits unheated hopper residence to 30 minutes.
How do I know if my resin is dry enough?
Measure it. A loss-in-weight moisture analyzer works for most resins, but one producer notes no shop-floor weighing system reliably measures below about 0.05%. For tight targets such as 0.02% on polycarbonate or PBT, use Karl Fischer or the carbide method, and set the analyzer temperature for the specific resin.
What are the signs of molding wet resin?
Splay or silver streaks, bubbles and voids, nozzle drool and stringing (especially nylon), lower melt viscosity that causes flash, and in PC, PBT and PET, brittle parts that can look perfect. If a part cracks in testing but looks fine, check moisture before anything else.
Values were compiled from resin producers’ published drying and processing guides. Confirm against the data sheet for the exact grade you are running.
If you are qualifying a new grade and want the drying window confirmed against the actual data sheet, send us the grade. A polymer chemist reviews it and we will tell you what the producer specifies.