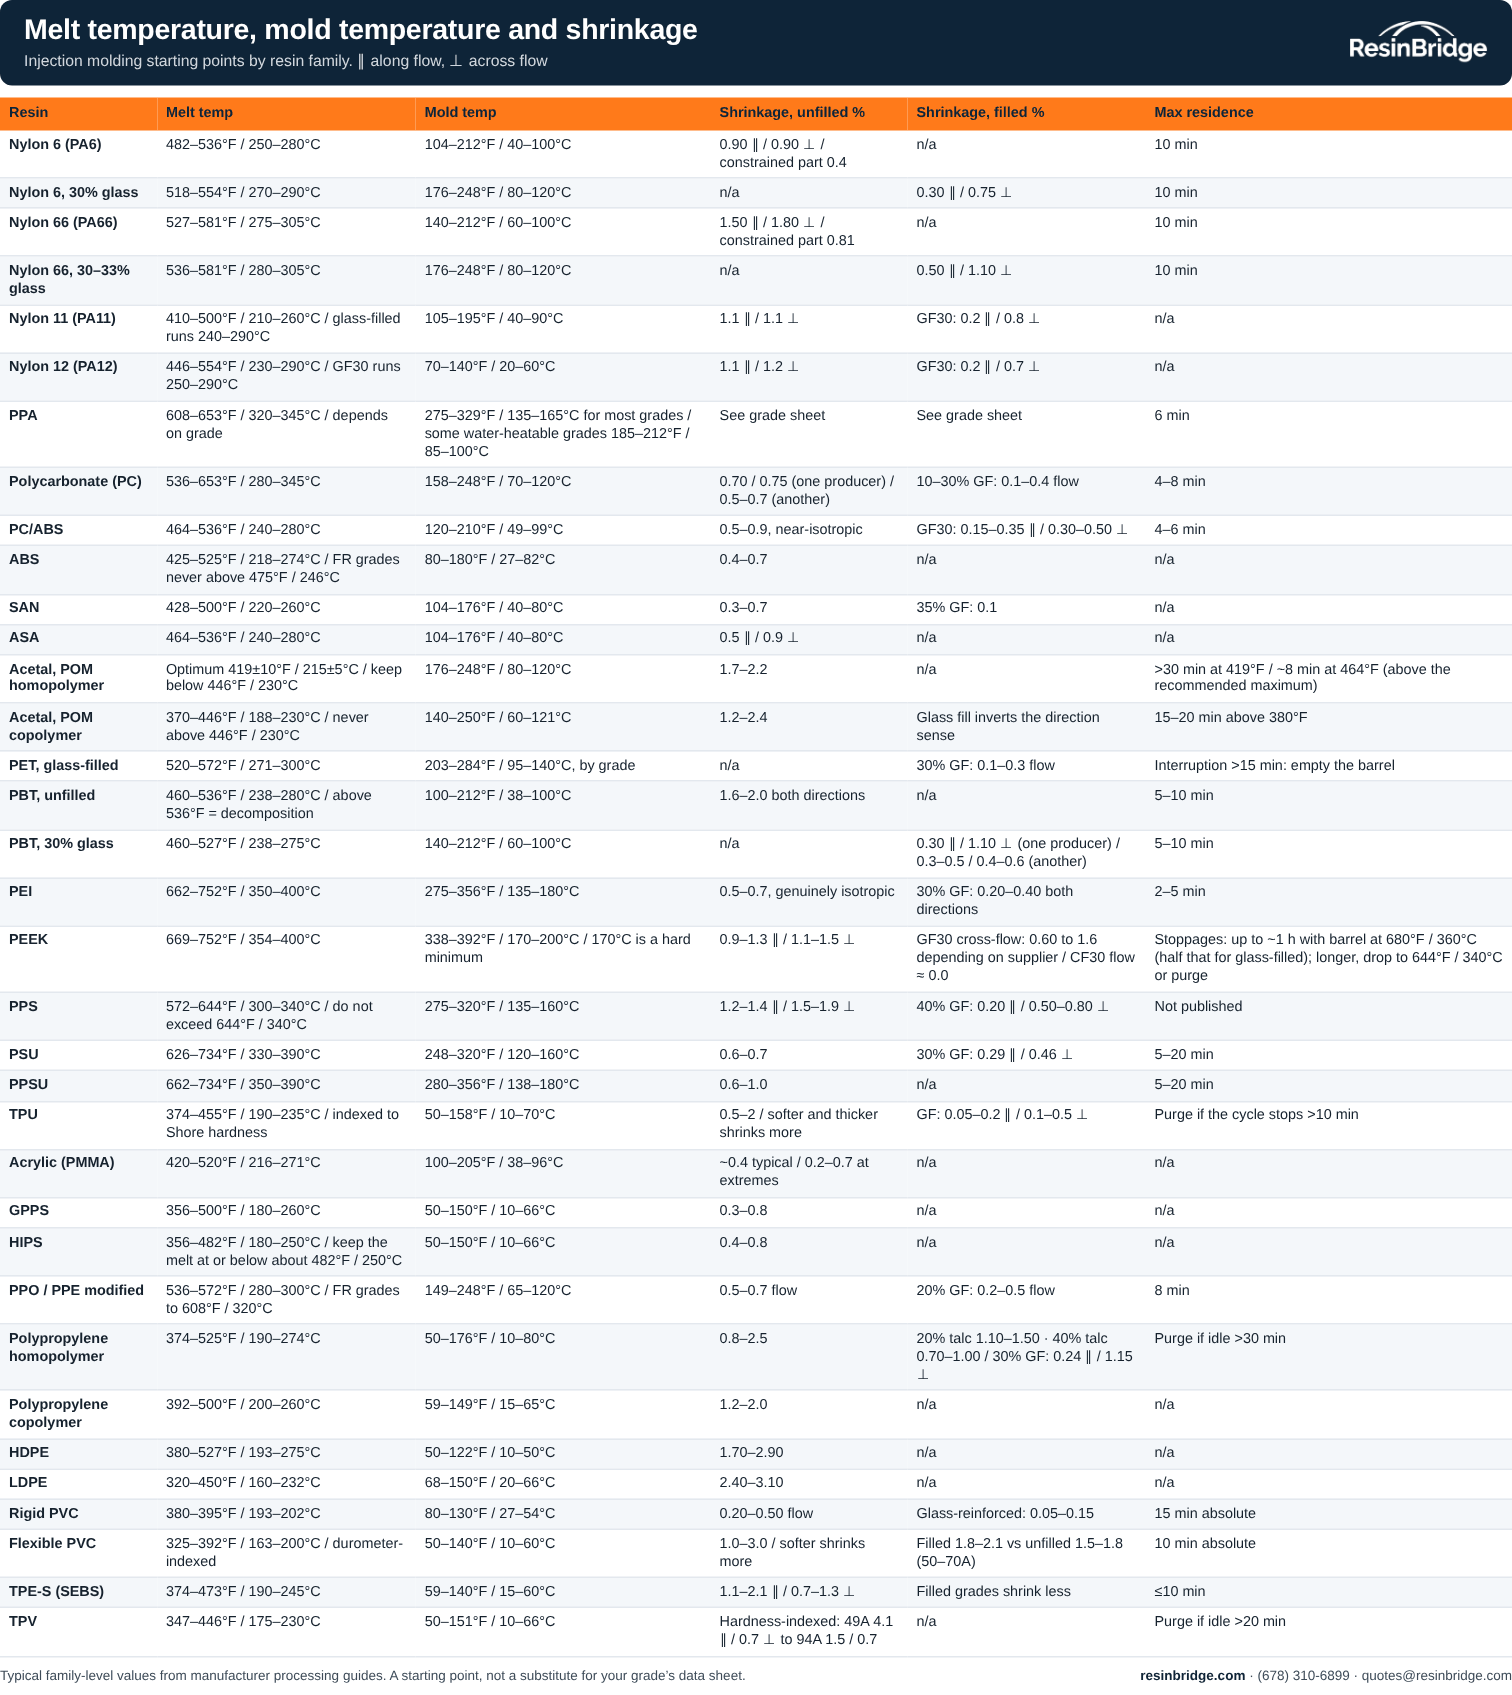
Mold shrinkage, melt temperature, mold temperature and barrel residence time for 35 thermoplastic families, from manufacturer processing guides and technical data sheets. Shrinkage is shown along and across flow where they differ, because glass-filled grades can shrink several times more across flow than along it. A source note is at the bottom. Companion to our resin drying chart.
Put the numbers to work with the cooling time, residence time and clamp tonnage calculators, or print this chart for the press.
How to read this chart
These are family-level typical values from manufacturer processing guides. They are a starting point for a process and a sanity check on a data sheet, not a substitute for the sheet on the grade you are actually running. Where suppliers disagree materially, both figures appear.
Processing parameters by resin
Scroll the table sideways to see all columns
| Resin | Melt temp | Mold temp | Shrinkage, unfilled % | Shrinkage, filled % | Max residence | Notes |
|---|---|---|---|---|---|---|
| Nylon 6 (PA6) | 482–536°F / 250–280°C | 104–212°F / 40–100°C | 0.90 ∥ / 0.90 ⊥ constrained part 0.4 | n/a | 10 min | Mold temp is the biggest disagreement on this chart: one producer says 40–60°C, another 80–100°C. Nylon 6 & 66 grades › |
| Nylon 6, 30% glass | 518–554°F / 270–290°C | 176–248°F / 80–120°C | n/a | 0.30 ∥ / 0.75 ⊥ | 10 min | 2.5× anisotropic. Glass-filled nylon grades › |
| Nylon 66 (PA66) | 527–581°F / 275–305°C | 140–212°F / 60–100°C | 1.50 ∥ / 1.80 ⊥ constrained part 0.81 | n/a | 10 min | ISO plaque value is roughly double the real constrained-part value. Nylon 6 & 66 grades › |
| Nylon 66, 30–33% glass | 536–581°F / 280–305°C | 176–248°F / 80–120°C | n/a | 0.50 ∥ / 1.10 ⊥ | 10 min | 2.2× anisotropic. Glass-filled nylon grades › |
| Nylon 11 (PA11) | 410–500°F / 210–260°C glass-filled runs 240–290°C | 104–194°F / 40–90°C | 1.1 ∥ / 1.1 ⊥ | GF30: 0.2 ∥ / 0.8 ⊥ | n/a | 4× anisotropy on GF30, the largest in the nylons. Nylon 11 & 12 grades › |
| Nylon 12 (PA12) | 446–554°F / 230–290°C GF30 runs 250–290°C | 68–140°F / 20–60°C | 1.1 ∥ / 1.2 ⊥ | GF30: 0.2 ∥ / 0.7 ⊥ | n/a | Melt temp is grade-driven, not family-driven. Nylon 11 & 12 grades › |
| PPA | 608–653°F / 320–345°C depends on grade | 275–329°F / 135–165°C for most grades some water-heatable grades 185–212°F / 85–100°C | See grade sheet | See grade sheet | 6 min | Size the shot at 30–70% of barrel capacity. PPA grades › |
| Polycarbonate (PC) | 536–653°F / 280–345°C | 158–248°F / 70–120°C | 0.70 / 0.75 (one producer) 0.5–0.7 (another) | 10–30% GF: 0.1–0.4 flow | 4–8 min | Residence has a real lower bound too: under 4 min gives an under-compounded melt. Polycarbonate (PC) grades › |
| PC/ABS | 464–536°F / 240–280°C | 120–210°F / 49–99°C | 0.5–0.9, near-isotropic | GF30: 0.15–0.35 ∥ / 0.30–0.50 ⊥ | 4–6 min | One producer publishes identical parallel and normal values. PC/ABS grades › |
| ABS | 425–525°F / 218–274°C FR grades never above 475°F / 246°C | 80–180°F / 27–82°C | 0.4–0.7 | n/a | n/a | Three suppliers agree on shrinkage and disagree by 55°F on mold temp. ABS grades › |
| SAN | 428–500°F / 220–260°C | 104–176°F / 40–80°C | 0.3–0.7 | 35% GF: 0.1 | n/a | ASA / SAN grades › |
| ASA | 464–536°F / 240–280°C | 104–176°F / 40–80°C | 0.5 ∥ / 0.9 ⊥ | n/a | n/a | The widely quoted “0.5–0.9%” is the two directions, not a grade range. ASA is not isotropic. ASA / SAN grades › |
| Acetal, POM homopolymer | Optimum 419±10°F / 215±5°C keep below 446°F / 230°C | 176–248°F / 80–120°C | 1.7–2.2 | n/a | >30 min at 419°F ~8 min at 464°F (above the recommended maximum) | Hot-runner steel capped at 374°F / 190°C. Acetal (POM) grades › |
| Acetal, POM copolymer | 370–446°F / 188–230°C never above 446°F / 230°C | 140–250°F / 60–121°C | 1.2–2.4 | Glass fill inverts the direction sense | 15–20 min above 380°F | Suppliers disagree 6× on residence. See the decomposition warning below. Acetal (POM) grades › |
| PET, glass-filled | 520–572°F / 271–300°C | 203–284°F / 95–140°C, by grade | n/a | 30% GF: 0.1–0.3 flow | Interruption >15 min: empty the barrel | Engineering injection grades of PET are almost always glass- or mineral-filled. Bottle-resin numbers do not apply to them. PET / PBT grades › |
| PBT, unfilled | 460–536°F / 238–280°C above 536°F = decomposition | 100–212°F / 38–100°C | 1.6–2.0 both directions | n/a | 5–10 min | ~70°F supplier conflict on mold temp. PET / PBT grades › |
| PBT, 30% glass | 460–527°F / 238–275°C | 140–212°F / 60–100°C | n/a | 0.30 ∥ / 1.10 ⊥ (one producer) 0.3–0.5 / 0.4–0.6 (another) | 5–10 min | The anisotropy ratio itself varies 3× between suppliers, 1.3:1 to 3.7:1. Glass-filled PBT grades › |
| PEI | 662–752°F / 350–400°C | 275–356°F / 135–180°C | 0.5–0.7, genuinely isotropic | 30% GF: 0.20–0.40 both directions | 2–5 min | Isotropic even at 30% glass. Unusual and useful. PEI grades › |
| PEEK | 669–752°F / 354–400°C | 338–392°F / 170–200°C 170°C is a hard minimum | 0.9–1.3 ∥ / 1.1–1.5 ⊥ | GF30 cross-flow: 0.60 to 1.6 depending on supplier CF30 flow ≈ 0.0 | Stoppages: up to ~1 h with barrel at 680°F / 360°C (half that for glass-filled); longer, drop to 644°F / 340°C or purge | Largest supplier spread on the chart. Do not average values from different producers. PEEK / PEK grades › |
| PPS | 572–644°F / 300–340°C do not exceed 644°F / 340°C | 275–320°F / 135–160°C | 1.2–1.4 ∥ / 1.5–1.9 ⊥ | 40% GF: 0.20 ∥ / 0.50–0.80 ⊥ | Not published | Avoid 190–260°F / 88–127°C mold temp: unpredictable crystallinity. PPS grades › |
| PSU | 626–734°F / 330–390°C | 248–320°F / 120–160°C | 0.6–0.7 | 30% GF: 0.29 ∥ / 0.46 ⊥ | 5–20 min | Filled sulfones are not isotropic, despite blanket claims to the contrary. PSU / PPSU grades › |
| PPSU | 662–734°F / 350–390°C | 280–356°F / 138–180°C | 0.6–1.0 | n/a | 5–20 min | PSU / PPSU grades › |
| TPU | 374–455°F / 190–235°C indexed to Shore hardness | 50–158°F / 10–70°C | 0.5–2 softer and thicker shrinks more | GF: 0.05–0.2 ∥ / 0.1–0.5 ⊥ | Purge if the cycle stops >10 min | 60–80A runs 190–205°C; 98A–74D runs 215–235°C. A soft grade at the family maximum will degrade. TPU grades › |
| Acrylic (PMMA) | 420–520°F / 216–271°C | 100–205°F / 38–96°C | ~0.4 typical 0.2–0.7 at extremes | n/a | n/a | Add 0.1–0.3% for humidity expansion in service, most of the shrinkage budget. Acrylic (PMMA) grades › |
| GPPS | 356–500°F / 180–260°C | 50–150°F / 10–66°C | 0.3–0.8 | n/a | n/a | GPPS & HIPS grades › |
| HIPS | 356–482°F / 180–250°C keep the melt at or below about 482°F / 250°C | 50–150°F / 10–66°C | 0.4–0.8 | n/a | n/a | GPPS & HIPS grades › |
| PPO / PPE modified | 536–572°F / 280–300°C FR grades to 608°F / 320°C | 149–248°F / 65–120°C | 0.5–0.7 flow | 20% GF: 0.2–0.5 flow | 8 min | Published mold-temperature guidance is not consistent; follow the grade sheet. PPO / PPE grades › |
| Polypropylene homopolymer | 374–525°F / 190–274°C | 50–176°F / 10–80°C | 0.8–2.5 | 20% talc 1.10–1.50 · 40% talc 0.70–1.00 30% GF: 0.24 ∥ / 1.15 ⊥ | Purge if idle >30 min | Glass-filled PP is the worst anisotropy of the filled grades here, about 5:1 in this example. Polypropylene (PP) grades › |
| Polypropylene copolymer | 392–500°F / 200–260°C | 59–149°F / 15–65°C | 1.2–2.0 | n/a | n/a | Measured 24 h after molding. PP homo & impact copolymer grades › |
| HDPE | 380–527°F / 193–275°C | 50–122°F / 10–50°C | 1.70–2.90 | n/a | n/a | About a 145°F supplier spread on melt, and opposite mold-temp advice. Both positions are defensible. HDPE injection grades › |
| LDPE | 320–450°F / 160–232°C | 68–150°F / 20–66°C | 2.40–3.10 | n/a | n/a | Polyethylene (PE) grades › |
| Rigid PVC | 380–395°F / 193–202°C | 80–130°F / 27–54°C | 0.20–0.50 flow | Glass-reinforced: 0.05–0.15 | 15 min absolute | Degrades to gaseous HCl. Neutralize tools daily. PVC grades › |
| Flexible PVC | 325–392°F / 163–200°C durometer-indexed | 50–140°F / 10–60°C | 1.0–3.0 softer shrinks more | Filled 1.8–2.1 vs unfilled 1.5–1.8 (50–70A) | 10 min absolute | Soft PVC melt should not exceed 392°F / 200°C. PVC grades › |
| TPE-S (SEBS) | 374–473°F / 190–245°C | 59–140°F / 15–60°C | 1.1–2.1 ∥ / 0.7–1.3 ⊥ | Filled grades shrink less | ≤10 min | TPE / TPV grades › |
| TPV | 347–446°F / 175–230°C | 50–151°F / 10–66°C | Hardness-indexed: 49A 4.1 ∥ / 0.7 ⊥ to 94A 1.5 / 0.7 | n/a | Purge if idle >20 min | Hardness changes the anisotropy, not just the magnitude. Cross-flow stays flat. TPE / TPV grades › |
Use this chart on your site or print it
Molding schools, dryer and auxiliary equipment dealers, and plants are welcome to put this chart on their own site or intranet. Paste the code below into any page. The chart stays current when we update it, and the credit link has to stay in place. Please don’t change the numbers.
Prefer paper? Download the printable PDF. Want to link instead? Use https://resinbridge.com/insight-processing-parameters.
Eight things worth knowing before you use these numbers
1. Amorphous and semi-crystalline behave differently, with two exceptions
Amorphous resins (PC, ABS, SAN, PS, PMMA, PEI, sulfones, modified PPE) mostly sit in a narrow band of about 0.3–1.0% and are close to isotropic. Semi-crystalline resins (nylon, acetal, PBT, PP, PE, PPS, PEEK) shrink about 1–3% unfilled and are direction- and crystallinity-sensitive. Two exceptions catch people out: ASA is not isotropic: the commonly quoted “0.5–0.9%” is the two directions, not a grade range. And filled sulfones are not isotropic either, despite blanket statements to the contrary; one producer’s 30% glass PSU is 0.29 along flow and 0.46 across.
2. Acetal decomposition is the highest-consequence line on this page
One producer’s guide: acetal copolymer should never be heated above 446°F (230°C), nor remain above 380°F for more than 15 minutes without purging. Beyond that the resin degrades and releases formaldehyde, and if venting is inadequate, pressure builds in the equipment. A homopolymer guide: decomposition is almost entirely to gaseous products, so pressure build-up can be rapid.
3. Residence time and melt temperature are one parameter, not two
Every supplier that publishes seriously publishes a curve, not a single number. One guide puts it directly: residence time should be as short as possible when molding near the maximum suggested melt temperature. A “max residence” figure is only valid at the low end of the melt range. A polycarbonate guide adds the opposite caution: below about 4 minutes you get an insufficiently compounded melt.
4. Mold temperature sets crystallinity, and the trade runs both ways
Mold shrinkage rises with mold temperature; post-mold shrinkage falls. Cold-molded semi-crystalline parts measure fine out of the press and then move in service. Three specifics: PEEK needs a 170°C minimum tool surface or you get amorphous parts that crystallize later above Tg. PPS has a forbidden band: 190–260°F yields unpredictable crystallinity and should be avoided. And injection-grade PET needs a hot mold, the opposite of preform tooling, which is one more reason never to read bottle-resin numbers across. For acetal homopolymer, annealing will not rescue a cold-molded part. It produces uncontrolled deformation instead.
5. Measure at 24 hours minimum, 48 for polyolefins
One polyolefin producer: a polyolefin part reaches about 90% of total shrinkage after 48 hours, and shrinkage continues for days if parts are packed hot. Another producer anchors its published values to 24 hours after molding. Force-cooling parts to measure sooner (in a fridge or under water) measures thermal contraction, not shrinkage.
6. Hold pressure and gate freeze set the number as much as the resin does
One producer’s guide: shrinkage begins the moment cavity pressure reaches atmospheric, and that point moves with the holding-pressure profile, so shrinkage can be influenced directly. Another notes polystyrene shrinkage may be effectively zero in zones under high follow-up pressure. Every published figure is conditional on a specific plaque geometry and set of conditions.
7. Nylon and acrylic grow after molding
One nylon guide: in a well-molded nylon part of moderate wall thickness, expansion from water absorption dominates the shrinkage from increasing crystallinity. Acrylic does the same: one producer publishes corrections to be added: +0.1% at 40% RH, +0.2% at 65%, +0.3% at 80%. On a 0.4% nominal shrinkage that is most of the budget.
8. ISO and ASTM values are not interchangeable
ISO 294-4 and ASTM D955 use different specimens, hold conditions and timing, and reference thicknesses differ (2 mm vs 3.2 mm). One producer publishes ISO plaque shrinkage of 1.50/1.80% for unfilled PA66 but a constrained real-part value of 0.81%, roughly half. Another says it flatly: shrinkage values measured on standard ASTM or ISO test bars should be used for material comparison only, not for tool design.
Some parameters aren’t indexed to the resin at all
A family-level row will mislead you in four cases. TPU melt temperature tracks Shore hardness: 190–205°C at 70A versus 215–235°C at 74D, so a soft grade run at the family maximum will degrade. Flexible PVC melt temperature and shrinkage both track durometer. TPV flow-direction shrinkage falls from 4.1% at 49A to 1.5% at 94A while cross-flow stays flat near 0.7%. Hardness changes the anisotropy itself. And PA12 melt temperature is grade-driven: unfilled runs 230°C, 30% glass runs 270°C.
One thing that surprised us
Engineering injection grades of PET are almost always glass- or mineral-filled. Bottle-resin numbers do not apply to them. If you find an “unfilled injection PET” shrinkage figure on a chart somewhere, it was almost certainly borrowed from bottle resin, which is processed under completely different conditions.
Common questions
What is the shrinkage rate of glass-filled nylon?
It depends on direction, and a single number is misleading. Glass fibers align with flow and restrain shrinkage along it. PA66 with 30–33% glass shrinks about 0.50% along flow and 1.10% across it, a 2.2 to 1 ratio. Glass-filled polypropylene is about 5 to 1 in the example on this chart. Use both values for tool design.
Why does glass-filled plastic shrink less in the flow direction?
The fibers orient with the melt front and restrain contraction along that axis, while across the flow the polymer shrinks nearly unrestrained. That is why fiber-filled semi-crystalline resins are strongly anisotropic, and why gate location moves dimensions more than any process change on carbon-filled PEEK or PEI.
How long can acetal stay in the barrel?
Suppliers disagree by about six times. One producer specifies never above about 230°C / 446°F, and no more than 15 minutes above about 193°C / 380°F without purging. Another gives 60 minutes at 200°C / 392°F, 30 at 210°C / 410°F and 10 at 230°C / 446°F. Overheated acetal decomposes to formaldehyde gas and can pressurize the barrel.
When should molded parts be measured for shrinkage?
At least 24 hours after molding, and 48 hours for polyolefins. One polyolefin producer notes a part reaches only about 90% of total shrinkage at 48 hours. Do not force-cool parts to measure sooner: that measures thermal contraction, not shrinkage.
Can PVC and acetal run in the same machine?
Not without a thorough purge between them. Producer guidance warns that PVC and acetal must never contact each other at processing temperature. The reaction accelerates and can lead to a violent release of gases.
Can I run a different resin in the same mold?
Sometimes, if the new resin shrinks about the same in both flow directions and runs at similar temperatures. Compare the shrinkage rows on this chart first, then trial it. See running a different resin in your mold for common swaps.
Where do these numbers come from?
From resin producers’ published processing guides and data sheets, summarized by resin family. Grades within a family vary, so treat the chart as a starting point and confirm against the data sheet for the exact grade you run.
Values were compiled from resin producers’ published drying and processing guides. Confirm against the data sheet for the exact grade you are running.
Qualifying a grade and want these confirmed against the producer’s current data sheet? Send us the grade. A polymer chemist reviews it.